+86 13638632902
 Jason@cleanroomequips.com


 MENU
Smoke is probably one of the most commonly misunderstood pollutants in air filtration engineering. Many facility managers treat smoke as though it was conventional dust – they buy a standard pleated filter and are surprised when they still have odors, haze and complaints.
The truth is that smoke is both a particulate pollution and gas-phase contamination issue. There is, therefore, a need for a number of separate filtration processes to be employed to deal with smoke effectively — which is why smoke odor filtration is engineered separately from particle capture.
This guide is intended to explain how smoke removal air filters work, why smoke air filters have to be HEPA filter for smoke, and through which processes activated carbon smoke filter work. It will also provide an overview of the selection, sizing and expected performance of smoke removal air filters.
In this guide you will also discover how DEIIANG manages its industrial smoke filtration – through a focus on media selection, contact time, pressure drop and monitoring performance rather than turning to filters only as a commodity item.
The Technical Challenge: The Concept of Smoke as a Mixture
Smoke is different from dirt. It is a dynamic system of aerosol that consists of solid matter, condensed water droplets, and a complex mix of gas. When you see smoke, you are actually seeing light being scattered by tiny particles — a fact that shapes tobacco smoke removal, wildfire response, and workshop fume control alike. The odor of smoke can be attributed to the presence of VOCs, acidic gases, and other aromatic substances which cannot be removed by a filter.
The distribution of particles in smoke depends on the type of fuel used, combustion temperature, condensation characteristics, and duration of time for which the smoke remains in the air. EACH of the different sources of smoke will have its own particle distribution. Therefore numerical figures should be considered for particular applications, and the figures should be verified with data from measurement or literature [1][6].
It is this mixed behavior that has made it necessary to have more than one stage since in this situation one stage is not effective for smoke removal and gas removal simultaneously. A particulate filter can remove the haze from the air, but it cannot completely remove the odor. A stage that contains only carbon is able to remove odor, but it cannot withstand soot particles and oils. It is necessary to specify effective smoke removal filters as systems.
Particulate matter and gas behave differently in the filter. Particulate matter is intercepted and diffused on the fiber surface, while gas is captured through adsorption. The following table explains the differences between contaminant types, and why an activated carbon smoke filter sits downstream of particulate media.
| Contaminant Type | Typical Nature | Examples in Smoke | Primary Filtration Technology | Standard Media |
|---|---|---|---|---|
| Solid particulates | Fine/ultrafine particles | Soot, ash, metal oxides/PM2.5 | Interception, impaction, diffusion | HEPA/high-efficiency fiberglass |
| Liquid droplets | Condensed aerosol | Oil mist, tar aerosol, condensed organics | Coalescence followed by drainage | Coalescing pre-filters |
| Gaseous VOCs | Molecular | Benzene, formaldehyde, acrolein | Physical adsorption | Activated carbon |
| Acid gases | Molecular | SO2, HCl, NOx | Chemisorption | Impregnated carbon |
| Odor compounds | Molecular, trace | Ammonia, mercaptans, amines | Adsorption | Activated carbon |
| Contaminant | Examples | Standard Media |
|---|---|---|
| Solid particulates | Soot, ash, PM2.5 | HEPA/fiberglass |
| Liquid droplets | Oil mist, tar aerosol | Coalescing pre-filter |
| Gaseous VOCs | Benzene, formaldehyde | Activated carbon |
| Acid gases | SO2, HCl, NOx | Impregnated carbon |
| Odor compounds | Ammonia, amines | Activated carbon |
The figure below explains how each filter stage is designed to capture different components of smoke — and why buyers asking "are there air filters specifically for smoke removal" get a qualified yes.
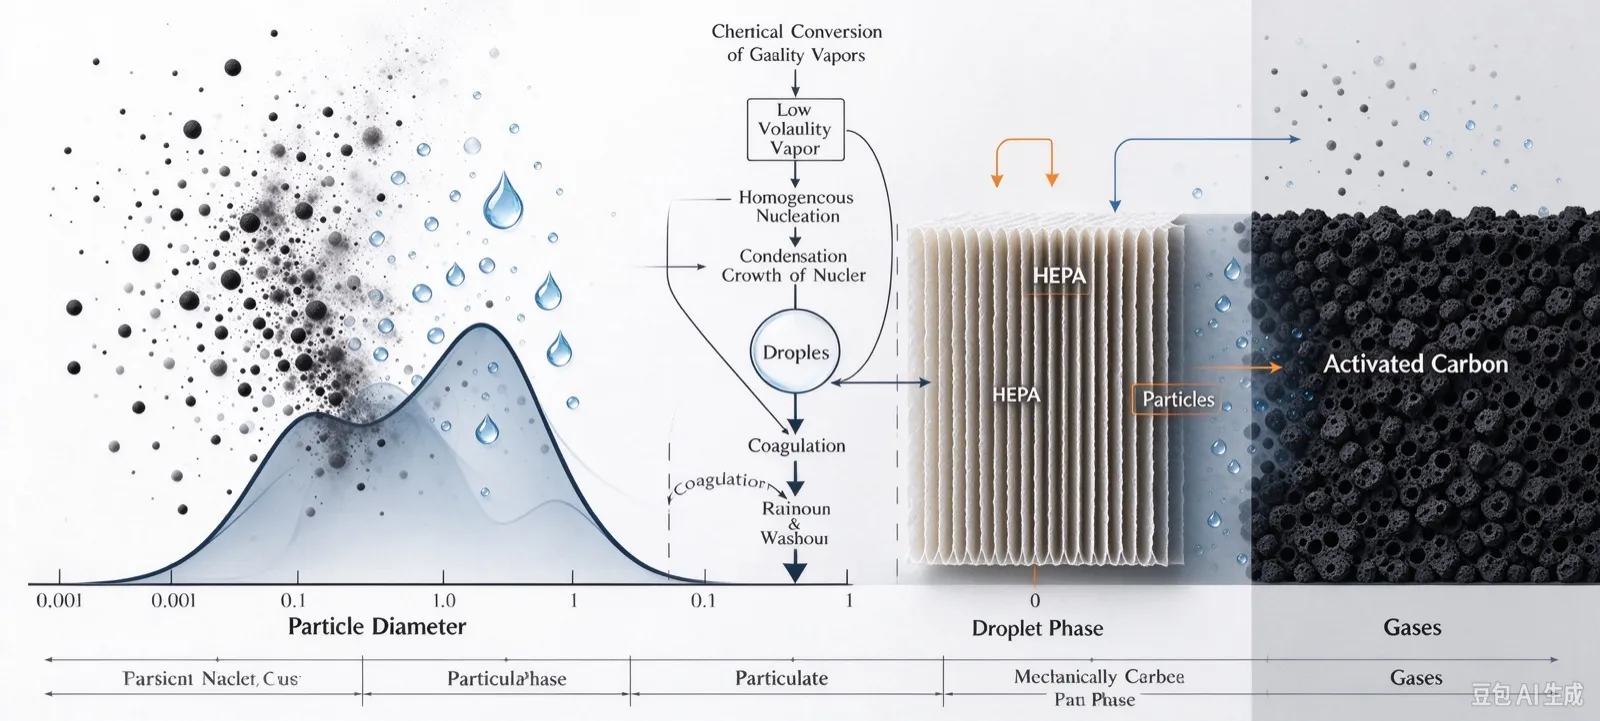
The diagram maps the three phases of smoke against the two main capture mechanisms. The particulate band is handled by mechanical filtration; the gas band requires adsorption media, so a HEPA filter for smoke alone cannot do the whole job.
Figure 1: Smoke composition mapped against filter capture mechanisms.
Which smoke type do you want to control?
Before selecting smoke control air filters, determine the source of the smoke. Wildfire smoke, tobacco smoke, welding fumes, soldering fumes, kitchen smoke, laser fume, and emissions from cleanroom processes have varying loadings of particles, gas composition, and requirements for safety and ventilation. A system that works effectively in one application may not work in another.
The table below serves as an initial guideline. It is only a useful screening method, not a final design template for industrial smoke filtration. Each application must comply with applicable local codes and establish compliance with occupational exposure limits.
| Smoke Sources | Primary Airborne Particles | Primary Airborne Gases | Recommended Filtration Stages | Airborne Source Capture Required? | Limitations |
|---|---|---|---|---|---|
| Smoke from Wildfires and Forest Fires | Fine and ultrafine combustion particles | Volatile organic compounds (VOCs), aldehydes, acrolein, and carbon monoxide | Pre-filters and HEPA filters | No | Although HEPA filters do not eliminate carbon monoxide, filter bypass and fit are important considerations. |
| Smoke from Cigars, Cigarettes and Pipes | Fine and ultrafine solid particles and tar aerosol | Volatile organic compounds (VOCs), nicotine, and aldehydes | Pre-filters and HEPA filters | Yes | Filtration will not entirely eliminate the risk of exposure to the smoke produced by cigars and cigarettes indoors. |
| Smoke from Welding Processes | Pollution and fine particulate welding fumes | Chlorinated VOCs (VOCs), nitrogen oxides (NOx) and metal vapors | Spark arrestors, pre-filters and HEPA filters | Yes | Aircraft must be evaluated on-site to determine airflow patterns. |
| Smoke from Soldering Processes | Dry contamination and fine particulate welding fume | Formaldehydes and VOCs | Pre-filters and HEPA filters | Yes | Filters become clogged with oily contamination and therefore fail to filter effectively. |
| Smoke from Cooking Processes | Grease or combustible hydrocarbons | Odors and VOCs | Pre-filters and HEPA filters | Yes | HEPA filters are not to be used as substitutes for the listed components. |
| Smoke Produced from Laser and Surgical Diagnostics | Fine and ultrafine particles | Volatile organic compounds (VOCs) | Pre-filters and HEPA filters | Yes | Proper local exhaust systems are required for treatment in individual cases. |
| Smoke from Specialized Overall Processes | Contaminants specific to particular processes | Acid gases and bases | Cartridge filters and either HEPA or ULPA filters | Yes | Classification of the particles does not ensure the removal of the gas. |
| Smoke Source | Key Gases | Stages | Source Capture |
|---|---|---|---|
| Wildfires | VOCs, CO | Pre-filter, HEPA | No |
| Tobacco | VOCs, nicotine | Pre-filter, HEPA | Yes |
| Welding | Ozone, NOx | Spark arrestor, pre-filter, HEPA | Yes |
| Soldering | Aldehydes, VOCs | Pre-filter, HEPA | Yes |
| Cooking | Odors, VOCs | Pre-filter, HEPA | Yes |
| Laser and surgical | VOCs | Pre-filter, HEPA | Yes |
| Specialized processes | Acid gases, bases | Cartridge, HEPA/ULPA | Yes |
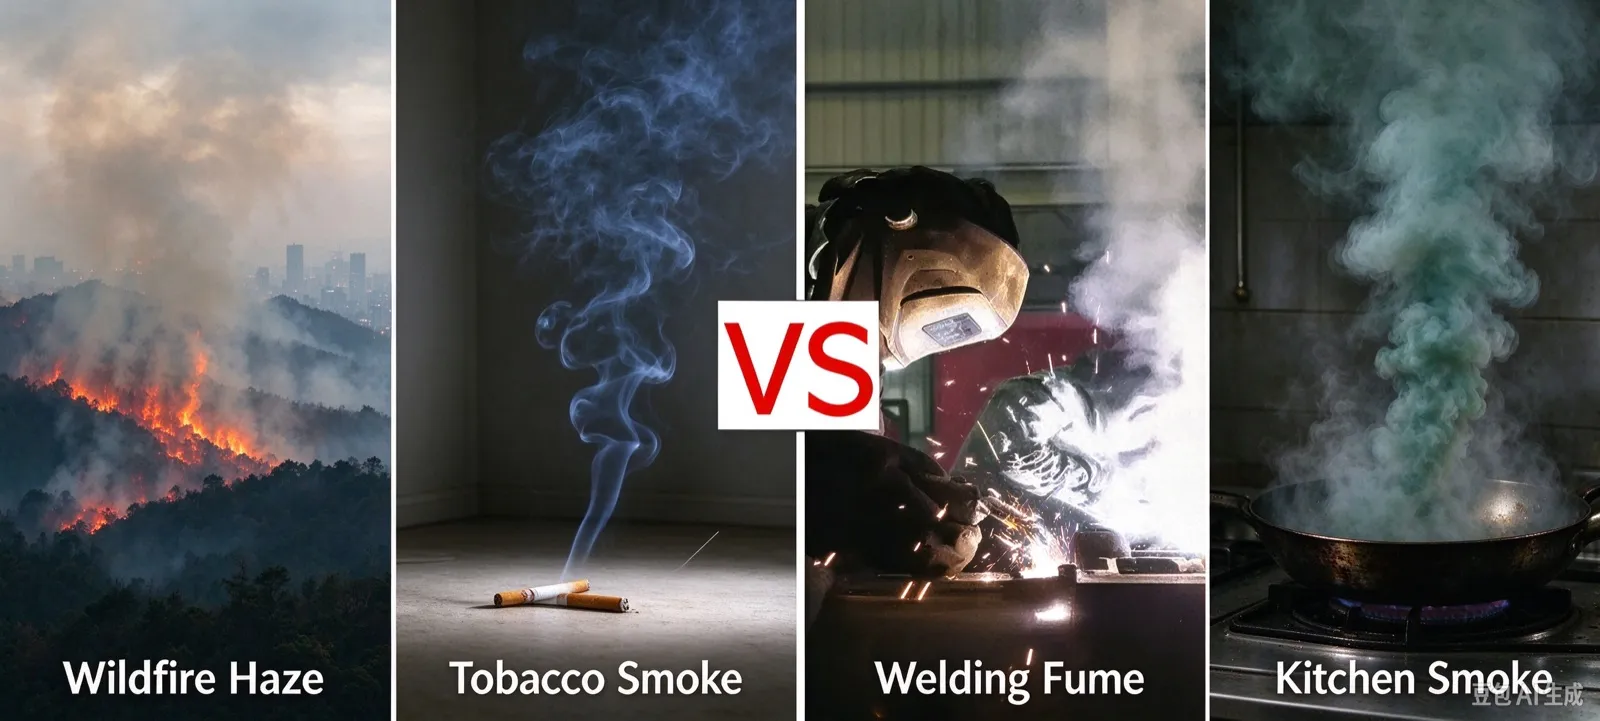
Wildfire haze arrives as a dilute regional aerosol, while tobacco, welding, and kitchen smoke are concentrated local sources that are best handled at the source.
Figure 2: Four smoke sources with very different behavior.
Filter-Selection Matrix
The matrix below provides guidance for determining the composition to use in a smoke-capture system. This matrix should be used only as a design tool.
| Application | Pre-filter | Particulate Stage | Gas Media | Recirculation | Monitoring |
|---|---|---|---|---|---|
| Forest Fires | Yes | HEPA | Activated Carbon | Yes | Indoor PM2.5, CO |
| Tobacco | Yes | HEPA | Treated Carbon | Limited | PM2.5, VOC screening |
| Soldering | Coalescing | HEPA | Activated Carbon | Yes | Pressure drop, VOC screen |
| Welding | Spark arrestor | HEPA | Treated Carbon | Limited | Pressure drop, fume screening |
| Kitchen | Grease filter | HEPA (protected) | Carbon | Limited | Pressure drop |
| Laser and Surgery | Yes | HEPA | Activated Carbon | Limited | Pressure drop |
| Combustion Exhaust | Yes | HEPA | Activated Carbon | Limited | Gas-specific monitoring |
| Application | Stages | Recirculation |
|---|---|---|
| Forest Fires | Pre-filter, HEPA, carbon | Yes |
| Tobacco | Pre-filter, HEPA, carbon | Limited |
| Soldering | Coalescing, HEPA, carbon | Yes |
| Welding | Spark arrestor, HEPA, carbon | Limited |
| Kitchen | Grease, HEPA, carbon | Limited |
| Laser/Surgery | Pre-filter, HEPA, carbon | Limited |
| Combustion Exhaust | Pre-filter, HEPA, carbon | Limited |
Following the Deiiang Multistage Approach
Since there isn't a single filter that does everything, all of the Deiiang engineers have designed smoke-abatement systems based upon the three-staged approach; that is, each stage makes use of and ensures that the prior stage protects the next one while maximizing the lifespan of the filter media. Incorporating a pre-filter, which is a fraction of the cost of a HEPA filter, can considerably extend the service life of the downstream system.
The underlying principle is simple: eliminate the larger and oily particles first, accumulate the smaller particles in the middle stage, and leave behind the vapor phase to be polished at the final stage — the staged logic behind every smoke removal air filter train. If any stage is not implemented, the downstream filter either blocks up, or breaks down early.
In the typical industrial cigarette smoke filter arrangement, there are three main stages:
- Pre-filter: This stage eliminates large particles of soot, dust, and oil, which helps prolong the life of the filters that follow.
- HEPA: This stage removes small smoke particles, including the sub-micron particles that create haze.
- Activated Carbon: Finally, gaseous and odor adsorbents are used to absorb any remaining undesirables.
In heavy oily smoke situations, Deiiang sometimes specifies the use of fiberglass filters with F5-F9 implementation as the initial filter. These filters perform to temperatures of 150°C, have a high capacity for dust load and come in common sizes of 592×592×381 mm.
In the case of new specifications, ISO16890 ePM1, ePM2.5, and ePM10 ratings must be used instead of EN779 grades. These values are often related with U.S. HEPA standards, and buyers should treat the MPPS figure as the true rating of a HEPA filter for smoke duty. On the contrary, the classification of H13 and H14 is commonly classified based on EN 1822 or ISO 29463 which is based on the MPPS performance [4]. The customers must verify standards applicable to the stated value.
Frames are either made from aluminum, galvanized steel, and stainless steel with PU two-component sealant and EVA hot-melt separators. Airflow is rated between 1000 to 2500 m³/h with a maximum temperature of 70 °C and maximum relative humidity of 80%. Each filter is subjected to a separate factory aerosol test.
In the gas phase, activated carbon smoke filters contain a deep carbon filter bed. Shallow carbon smoke panels are common errors in smoke filtration because the residence time is too short for proper adsorption.
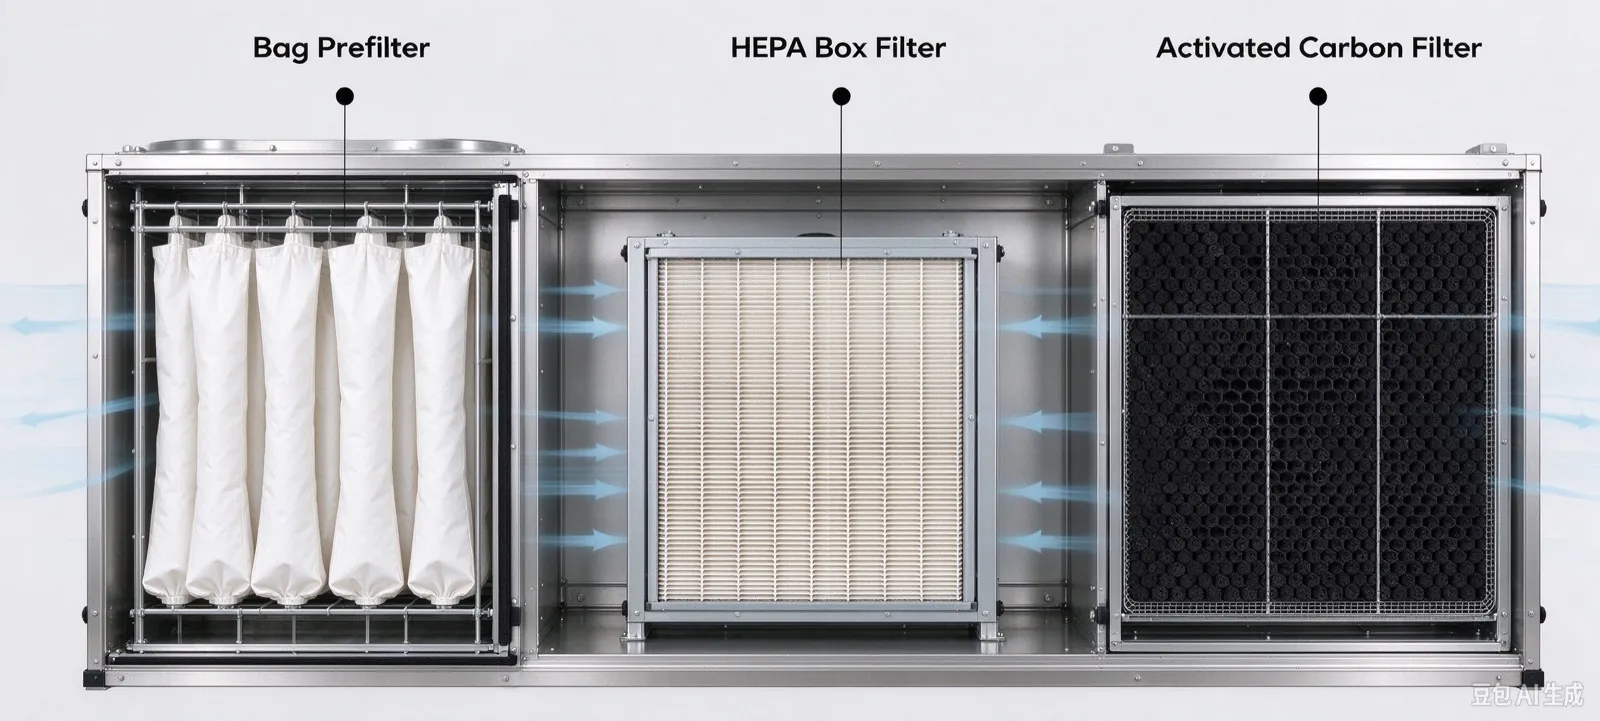
The staged train: bag pre-filter first, H13 HEPA second, activated carbon last. Each stage protects the next — the architecture used in every Deiiang smoke removal air filter.
Figure 3: Cutaway of a staged smoke abatement train.
Deiiang Product Data (verified)
The following table summarizes the critical product data information for verification. Values shown in this table are indicative unless stated otherwise. The buyers should ask for the relevant datasheet and test report.
| Product | Model / Grade | Nominal Airflow | Efficiency Basis | Temperature Limit | Humidity Limit | Test Documentation |
|---|---|---|---|---|---|---|
| Medium-effect fiberglass bag filter | F5–F9 (EN 779 legacy) | 2050 m³/h at 592×592×381 mm | 45–95% at 0.5 µm | 150°C | Consult datasheet | Factory batch test |
| DOP integrated HEPA filter | H13 | 1000–2500 m³/h | 99.97–99.99% at 0.3 µm | 70°C | 80% RH | Individual factory scan |
| DOP integrated HEPA filter | H14 | 1000–2500 m³/h | 99.995–99.999% at 0.3 µm | 70°C | 80% RH | Individual factory scan |
| Super high efficiency baffle-free filter | ULPA U15–U17 | Consult model | 0.12 µm rated | Consult model | Consult model | Individual factory scan |
| FFU module | Standard | Face velocity 0.45 m/s ±20% | HEPA or ULPA dependent | Consult model | Consult model | Factory test |
| Product | Grade | Efficiency | Temp Limit |
|---|---|---|---|
| Fiberglass bag filter | F5–F9 | 45–95% @0.5 µm | 150°C |
| HEPA filter | H13 | 99.97–99.99% @0.3 µm | 70°C |
| HEPA filter | H14 | 99.995–99.999% @0.3 µm | 70°C |
| ULPA filter | U15–U17 | 0.12 µm rated | Consult model |
| FFU module | Standard | 0.45 m/s ±20% | Consult model |
The chart below is a conceptual illustration of staged performance. It is not a product performance certificate.
Figure 3: Cutaway of a staged smoke abatement train — bag pre-filter, H13 HEPA, activated carbon. Certified stage performance should be confirmed with model-specific test reports.
Activated Carbon Selection: What Buyers Need to Specify
"Deep carbon bed" and contact time alone are not enough to specify a gas-phase filter. Buyers should request carbon mass, apparent density, adsorption capacity, bed area, and breakthrough data for the target gases. These are the specifications that separate a serious activated carbon smoke filter from a marketing label. The following checklist covers the minimum information required.
Engineering Features for System Design
Smoke filtering is a compromise between air changes and contact time — the two variables that decide whether a commercial air filtration system delivers. An air change rate defines what speed of purification is required, while the contact time affects the efficiency of carbon filtration. If one is too high, the other will be low.
Although air change rate can help in choosing an appropriate self-contained system, it can't show if source control is sufficient for immersion in mist. Instead, a system should use source-capture extraction instead of simple dilution — the first rule of industrial smoke filtration.
In order to provide 12 air changes per hour (ACH), it is necessary to have 1,200 × 12 = 14,400 m³/h of air flow within the ventilation system. This is a large system indeed.
The contact time for performance is calculated through the ratio between the carbon bed depth and the face velocity — a core concept in air filtration engineering. For a 50mm depth at a face velocity of 1.0m/s the contact time is measured to be 0.05 seconds, which is often deemed too short to allow for meaningful adsorption. The contact time for a 200mm depth at similar velocity is measured to be 0.2 seconds.
The engineering team at Deiiang typically starts with the performance specification range of 0.1 – 0.4 seconds; however, the specific time will depend upon the contaminant type, concentration, humidity and target outlet contaminant level.
The key steps in design include:
- Determining the design airflow as a function of room volume, contaminant generation rate and desired cleanliness or exposure level.
- Confirming source capture requirements and hood capture velocities before relying on room dilution for performance.
- Controlling static pressure drop through multiple filter stages by using the specific model performance data.
- Selecting the appropriate carbon type based on the actual target contaminant gases and the breakthrough criteria.
As a general rule, Deiiang uses Q = ACH × V / 3600 to size systems in metric m³/s. For example, the hood capture velocity for a welding bay with a contaminant generation rate of 0.5kg/hr would normally be estimated to be in the range of 0.5 – 1.0m/s. However, specific velocities vary based upon hood configuration and placement distance, air movement forces, temperature and energy produced by the work process. This must no doubt be confirmed by using recognized ventilation criteria and by performing smoke testing in a real working environment.
Budgeting for Pressure Drop
Budgeting for pressure drop can be somewhat complex in a three-stage set up. The chart that follows is a template for determining pressure budgets. Actual values should be taken from the certified product data.
| Stage | Filter Model | Max Airflow | Clean Resistance | Recommended Change-Out Resistance | Estimated Loaded Resistance | Fan Reserve |
|---|---|---|---|---|---|---|
| Pre-filter | F7 bag | 2,050 cfm | TBD as from data sheet | TBD | TBD | TBD |
| HEPA | H13 | 1,000–2,500 cfm | TBD as from data sheet | TBD | TBD | TBD |
| Carbon | Deep bed | Application Specific | TBD as from data sheet | TBD | TBD | TBD |
| Stage | Model | Data Required |
|---|---|---|
| Pre-filter | F7 bag | Clean and loaded resistance |
| HEPA | H13 | Clean and loaded resistance |
| Carbon | Deep bed | Clean and loaded resistance |
A common mistake in establishing a proper efficiency for a final stage is not taking into account the pressure load that it places on the fan — a classic air filtration engineering mistake. If the fan curve cannot provide the design airflow at the loaded pressure, there will be under-performance of the system, even if it is believed that the filter is doing as it should.
Fire, Explosion and Process Safety Screening
Industrial smoke filtration systems may be subject to the risk of sparks, hot particles, combustible materials, flammable vapors or chemical reaction. HEPA and carbon media may present opportunities for fire load if misapplied. Safety screening should be done before media selection.
Filter Efficiency vs Clean Room Effectiveness
Laboratory filter efficiency does not necessarily equal room contaminant control. Bypass leakage, poor mixing, continuous generation of source contamination, leakage from the ducts, short circuit airflow through the duct, and infiltration of outside air all compute on the actual performance as you may expect it.
Effective clean airflow is device airflow times single pass removal efficiency, multiplied by bypass and installation losses. The fact that a purifier has an airflow of 1000 m³ per hour and a collection efficiency of 99% in a single pass does not mean that a flow of 1000 m³ is obtained. The emission of 990 m³ of clean air equivalent is achieved, and for calculating the size of recycling devices, differences of this kind are important.
Testing after Commissioning
The commissioning process ensures that an installed system is working according to the original design, which is where most air filtration engineering assumptions get tested. Various verifications should be carried out and recorded.
Example Project: Deiiang Industrial Fume Extraction Project
The details of Deiiang Industrial Fume Extraction Project are presented below. Numerical values provided throughout this summary will be anonymized in some cases.
A precision electronics assembly has a 300 m² soldering and rework area in which the process emits rosin soldering fumes containing visible haze, odor, and VOC levels. The current single-stage filter system needs cleaning after every three weeks and does not control odor emissions, increasing the chances for the facility to fail its own air quality audit.
Details of the project:
- Nature of the project: Solder fume extraction and VOC abatement retrofit in the precision electronics assembly section with an area of 300 m².
- Year and location of the project: Asia-Pacific, 2025, client details withheld.
- Project Challenges: The oily rosin aerosol resulted in prompt filter plugging, ongoing odor complaints, limited available capacity of the fans, and the need for production to be maintained throughout the installation.
- Deiiang Approach: An advanced multi-stage air handling apparatus employing F7 glass fiber bag pre-filters (592 mm × 592 mm × 381 mm, each capable of handling up to 2050 m3/h of air), H13 DOP-integrated HEPA filters fitted with aluminum frames, and a coconut-shell deep-bed activated carbon filter with a contact period of approximately 0.2 seconds.
The retrofitting project reused an existing fan by minimizing the pressure drop in the pre-filters with a presumption of reduced filter bed pressure — a reminder that any HEPA filter for smoke lives or dies by pressure budget. Installation of the apparatus took place over the course of a weekend.
Verification of the multi-stage apparatus included determining the airflow, measuring the pressure, and conducting an on-site HEPA integrity test using an approved aerosol, plus carbon-stage checks that are standard in serious smoke removal air filter installations.
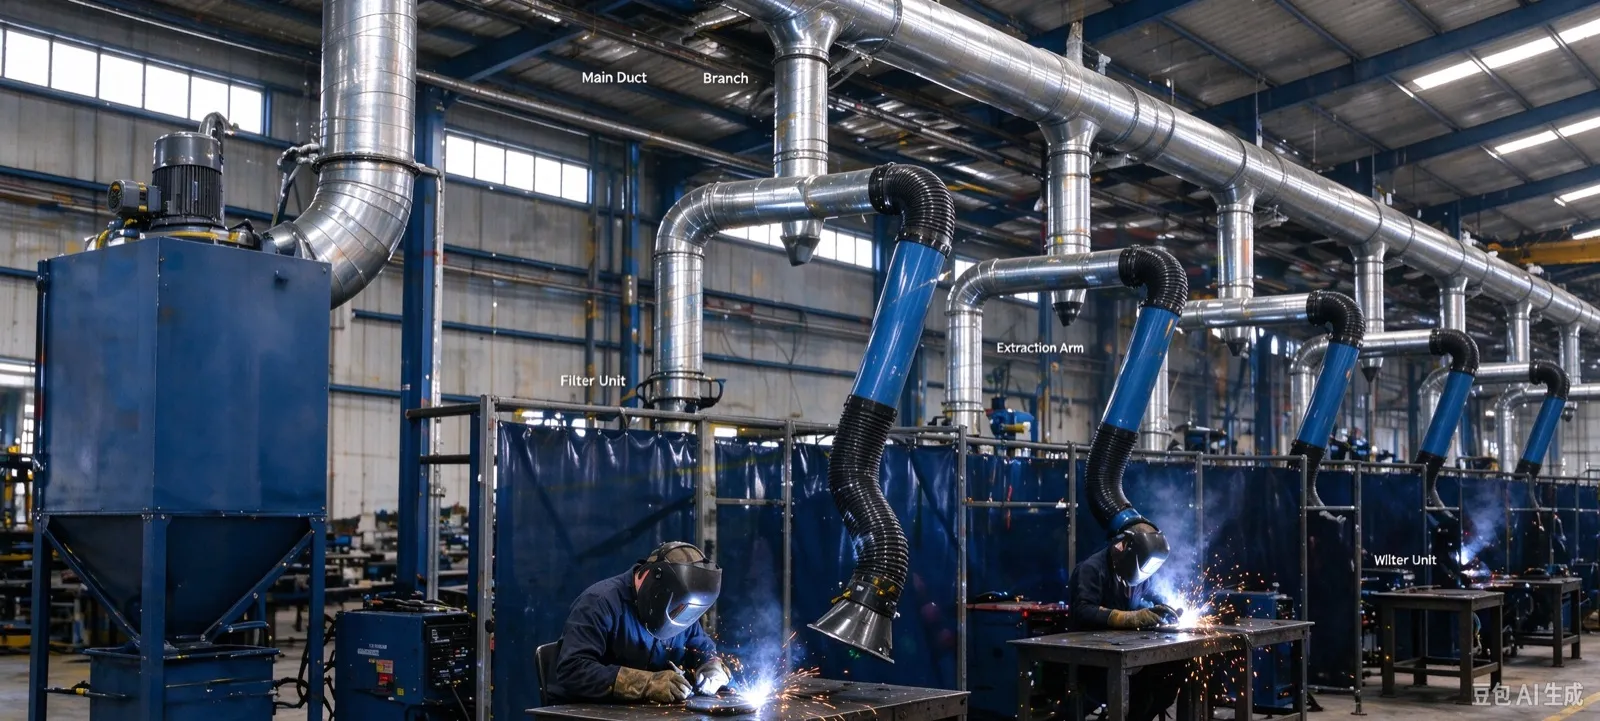
The installed system: labeled main duct, branch lines, flexible extraction arms, and the central filter unit.
Figure 4: Installed multistage smoke extraction system.
Comparison of Results pre and post Retrofit:
| Parameter | Pre retrofit | Post retrofit | Difference | Commentary |
|---|---|---|---|---|
| Particle count (≥0.5 µm, particles/m³) | 3.8 × 10⁷ | 2.1 × 10⁵ | ~99.4% decrease | Carried out using handheld particle counter and various locations after retrofitting |
| Detection and Quantification of VOCs (ppm isobutylene equivalent) | 4.2 | 0.3 | ~93% decrease | Based the detection and quantification of VOCs on PID with 10.6 eV lamp |
| Perceived intensity of odor (1-5 scale) | 4 | 1 | Decreased | Using informal panel; generation of data was not done in controlled manner |
| Change of filter frequency | ~3 weeks | ~14 weeks | ~4.7 times longer | Based on the trend of pressure-drop |
| Cleanliness status | Previously no classification | Now classified as project meeting specifications | Project meets objectives | Based on project acceptance test, not full iso 14644-1 classification |
| Parameter | Pre retrofit | Post retrofit | Difference |
|---|---|---|---|
| Particle count ≥0.5 µm | 3.8 × 10⁷ /m³ | 2.1 × 10⁵ /m³ | ~99.4% |
| VOC screening | 4.2 ppm | 0.3 ppm | ~93% |
| Odor intensity (1-5) | 4 | 1 | Decreased |
| Filter change interval | ~3 weeks | ~14 weeks | ~4.7× |
| Cleanliness status | Not classified | Meets project specs | Meets objectives |
The facility reported a reduction in the number of odor complaints as well as decrease in quantity of deployed filters in first year of adoption. Before conducting any cost-benefit analysis, the analysis of annual amount of filter, costs per unit filter, labor hours along with disposal cost and energy consumption have to be performed in conjunction with the adoption cost so that both of them could be analyzed.
This case study has been documented as project summary. Individuals considering similar industrial smoke filtration systems should request the anonymized reports of testing, photographs of deployment along with field deployment documentation.
When it Comes to Cleanroom Filtration
Certain facilities require both smoke suppression and cleanroom particle classification. Although connected, these are two different categories: cleanroom air filters are selected for particle concentration limits, not gas or odor load. cleanroom classification is according to iso 14644-1 and looks at airborne particles [2]. Therefore, it does not indicate that there is gas or odor elimination.
For applications with strict purity levels needed, such as wafer manufacturing or atomic research, Deiiang offers Super High Efficiency Baffle-Free Filters (ULPA U15-U17) with a rating of 0.12 µm using US HV ultrafine glass fiber paper. In cleanroom applications, FFU modules operating at 0.45 m/s ±20% are used for terminal filtration applications.
These products do not typically apply to smoke removal, but they can serve an important purpose if a smoke-free environment must also achieve stringent cleanliness classifications, where cleanroom air filters and smoke-duty carbon stages are specified side by side. Molecular contamination control design remains an independent requirement.
Design Factors Determined by Region and Locale
Deiiang uses local data to inform its designs because climatic, regulatory, energy cost, outside air quality, and ventilation practices shape conditions differently in each location. The following chart depicts how design will change, depending upon region.
| Region Type | High Design Factor | Implication for Filtration | Monitoring Priority |
|---|---|---|---|
| Humid Tropics | Moisture High | Humidity determines untreated carbon limitations; hydrophobic or impregnated is preferred | Humidity, pressure drop |
| Dry Industrial Region | Dust High | Prefilter capacity and replacement frequency greatly impacts filtration | Pressure drop, dust loading |
| Cold Climate | Outdoor Air Quality Low in Winter | Recirculation with filtration may be preferred | Indoor PM2.5, CO |
| Wildfire Region | Outdoor Air Quality high PM2.5 through Season | Building level HEPA and carbon; fit of filter is significant | Indoor PM2.5, CO |
| Region Type | Key Factor | Monitoring |
|---|---|---|
| Humid Tropics | High moisture | Humidity, pressure drop |
| Dry Industrial | High dust | Pressure drop, dust loading |
| Cold Climate | Low winter outdoor air quality | Indoor PM2.5, CO |
| Wildfire Region | Seasonal high PM2.5 | Indoor PM2.5, CO |
Regional data should come from a respected entity in the region and include year of data used. Deiiang does not publish the pollution or climate data of cities without citing the source.
Wildfire Smoke Problems
Smoke coming from wildfires is a prevalent reason why many buyers look for air filters that can eliminate smoke, and a properly specified wildfire smoke air filter is central to any building response. When it comes to the actions that can be taken to deal with this issue, there are a number of possible building response approaches.
This includes:
Smoke from Tobacco
Tobacco smoke removal is harder than most buyers expect: the smoke contains solid particles, tar aerosol, and gas mixtures. The use of filtration equipment restricted airborne particles and decreased the odor in rooms, but it cannot make smoking indoors safe. Preferably, smoking should be eliminated completely so that you do not expose anyone to smoking.
However, where filters are in use, the use of HEPA filter for smoke combined with an activated carbon smoke filter can also eliminate cigarette smoke and prevent the spread of smoke. This approach supports tobacco smoke removal and improves smoke odor filtration in enclosed spaces.
Commercial Applications
Commercial smoke problems differ from industrial ones. Kitchens, smoking lounges, hotels, warehouses, and offices each have distinct requirements for a commercial air filtration system — no single smoke removal air filter covers all of them.
| Application | Primary Issues | Suggested Solutions | Main Warning |
|---|---|---|---|
| Commercial kitchen | Smoke, humidity, smell | Code-approved grease removal and ventilation; carbon for odor elimination | HEPA is not an alternative to necessary kitchen exhaust components |
| Smoking lounge | Particles, gas, etc. | Source separation; supplementary HEPA and carbon | No means completely avoid risk |
| Accommodation | Odor and cigarette residue | Source control; HEPA and carbon in all affected areas | Surface residue will need cleaned, not just filtered |
| Warehouse | Diesel or process smoke | Source capture; ventilation; filtration as needed | CO and NOx demand specific controls |
| Office | Wildfire smoke and urban PM | HEPA and carbon at building level | Filter fit and bypass considerations |
| Application | Solution | Main Warning |
|---|---|---|
| Commercial kitchen | Grease removal, ventilation, carbon | HEPA not a substitute for exhaust components |
| Smoking lounge | Separation, HEPA, carbon | Risk cannot be fully avoided |
| Accommodation | Source control, HEPA, carbon | Surface residue needs cleaning |
| Warehouse | Source capture, ventilation | CO and NOx need specific controls |
| Office | Building-level HEPA and carbon | Filter fit and bypass matter |
What Smoke Filters Cannot Do
Prior to outlining any system, please be sure that expectations are in line with filtration's capabilities — and with what smoke odor filtration can and cannot adsorb.
- They do not remove carbon monoxide using standard HEPA or activated carbon.
- They do not replace oxygen.
- They do not ensure regulatory exposure compliance on their own.
- They do not get rid of third-hand smoke residues.
- They do not substitute for source control or required exhaust ventilation.
- They will not fix poor capture, duct leakage, or airflow short-circuiting.
Lifecycle Management and Performance Evaluation
Filters are consumables. They operate according to variable efficiency, and a filter working well at installation may fail within 6 months without drawing attention to itself. A smoke removal air filter system deteriorates in two ways: particulate steps load and create a greater pressure drop and carbon stages reach saturation and lose adsorption capacity with no visible indications.
Alarm setpoints must be determined according to manufacturer-recommendations with respect to final resistance, supply air available from fan, energy cost, process risk, and relevant operating experience and not general percentages applied universally. The practice of 60% or 80% is internally established and must be verified with regards to each process.
Best practices include:
- Install differential pressure gauges at every bank of filters and setpoints per manufacturer specific standards.
- Schedule regular air quality monitoring, because carbon breakthrough is not detectable visually.
- Prevent carbon media oversaturation to avoid breakthrough.
- Record baseline pressure readings during installation with weekly trending.
Sudden changes in pressure across HEPA filter may indicate seal or media failure; ascending pressure across a carbon filter signifies proper operation. It is preferable to monitor gases directly with gas analysis instead of relying on odor detection.
Monitoring Options for Carbon Breakthrough
PID meters have analyte-specific limitations. Utilizing odor detection as a primary alarm source is inappropriate and could potentially lead to a dangerous situation. Options for monitoring are outlined in the table below; for smoke odor filtration stages, direct gas measurement beats odor complaints every time.
| Contaminant | Monitoring Approach | Detection Range | Main Interference | Appropriate Alarm Method | Sampling Period |
|---|---|---|---|---|---|
| VOCs (general) | PID | ppm scale | Response ratios may be different | Trend and threshold | Weekly to monthly |
| Formaldehyde | Detector tube or dedicated sensor | ppb to ppm | Other kinds of aldehydes | Threshold warning | Monthly |
| Acidic gases | Detector tube or dedicated sensor | ppm scale | Humidity | Threshold warning | Monthly |
| Carbon monoxide | Electrochemical detector | ppm range | Other gases | Continuous alarm | Always |
| Smell | Evaluation through a panel | Qualitative | Adaptation | Complaint record | As needed |
| Contaminant | Method | Sampling Period |
|---|---|---|
| VOCs (general) | PID | Weekly to monthly |
| Formaldehyde | Detector tube or sensor | Monthly |
| Acidic gases | Detector tube or sensor | Monthly |
| Carbon monoxide | Electrochemical detector | Continuous |
| Smell | Panel evaluation | As needed |
You need to purchase monitoring equipment specific to the substances you are being tested for and calibrate them accordingly, especially for activated carbon smoke filter service life tracking.
Maintenance Safety and Waste Disposal
When loaded with particulate matter, the carbon filter could potentially contain hazardous metals or toxic pollutants. Thus, when handling, maintenance personnel need to be careful not to expose themselves.
Cost of Ownership
Purchasing facilities need to take into account the airflow and operating hours, clean and loaded pressure drop, fan efficiency and electricity price, and the costs associated with filters, labor, and replacement frequency. Costs resulting from disposal and downtime must also be considered.
Annual energy consumption, annual consumables together with total ownership cost estimates for five years should be provided for all outputs and their assumptions provided — standard practice in industrial smoke filtration procurement. Estimated savings, however, is not to be regarded as guaranteed savings.
Lifecycle Replacement Planning
The various replacements cannot be based only on calendar time schedules alone. In places where high smoke loads are being dealt with 24/7, it may be necessary to change pre-filters every month and carbon filters quarterly. In places with low workload, time duration may be extended.
The variables are concentration of contaminants, volume of air, humidity and nature of smoke chemically. Special focus should be laid on humidity since it reduces the adsorption capacity of the activated carbon — a key derating factor when specifying any activated carbon smoke filter. Where humidity is high, hydrophobic or impregnated carbon grades are utilized.
Conclusion
Smoke removal cannot be treated as a filter purchase. It can be treated as an engineering problem whose answer is sought for. The answer to the issue "Do we have smoke removal filters?" is yes when systems are coordinated. A HEPA filter for smoke deals with particulate phase while an activated carbon smoke filter deals with gas and odour. Pollutants are pre-filtered using an appropriate pre-filter and then purified. When the system is designed appropriately, then there is no guessing involved.
If your facility is experiencing visual smoke, offending odors, or filter replacement too often, it probably has to do with the incompatibility of the smoke and the filtration stages. In most cases the fix is either a proper HEPA filter for smoke upgrade or an added activated carbon smoke filter stage. The engineers at Deiiang use localized information and measurements to size each stage of the system properly.
No matter if you need a commercial air filtration system for the kitchen of a restaurant, an industrial smoke filtration system for a welding workshop, or a wildfire smoke air filter strategy for a large facility, they apply that same air filtration engineering discipline.
When making contact with Deiiang for a consultation, please provide:
- The source process and schedule.
- Measured gas and particle concentrations, if possible.
- The humidity and temperature.
- Exhaust or recirculation need.
- Available static pressure and current fan curve.
- Electrical supply and installation space.
- Applicable regulations and desired outlet concentration.
Now you have the first step to finding a real solution.
References
- ISO 16890-1:2016 — Air filters for general ventilation — Part 1: Technical specifications, requirements, and classification system based on the efficiency of the particulate matter (ePM). https://www.iso.org/standard/57835.html
- iso 14644-1:2015 — Clean rooms and other controlled environments — Part 1: Classification of air cleanliness by concentration of particles. https://www.iso.org/standard/53394.html
- EN 779:2012 — Particulate air filters for general ventilation — Determination of the performance of filtration. (Replaced by ISO 16890 in several areas.) https://www.en-standard.eu/bs-en-779-2012-particulate-air-filters-for-general-ventilation-determination-of-performace-of-filtration/
- ISO 29463 — High efficiency filters and filter media for particulate removal in air. https://www.iso.org/standard/69363.html
- ASHRAE Standard 52.2 — Method of testing general ventilation air cleaning devices for particle removal efficiency. https://www.ashrae.org/technical-resources/bookstore/standard-52-2
- EPA — Wildfire smoke and indoor air quality. https://www.epa.gov/indoor-air-quality-iaq/wildfires-and-indoor-air-quality
- NIOSH — Control of smoke from laser/electrosurgical procedures. https://www.cdc.gov/niosh/docs/hazardcontrol/hc11.html
- ASTM D2854 — Standard test method for the apparent density of activated carbon. (Note: only the apparent density is discussed and does not include adsorption.) https://www.astm.org/d2854-09r19.html
- IEST-RP-CC001 — HEPA and ULPA filters. https://www.iest.org/Standards-RPs/Recommended-Practices/IEST-RP-CC001