+86 13638632902
 Jason@cleanroomequips.com


 MENU
In the realm of cleanroom technology, maintaining a controlled environment is crucial for industries such as pharmaceuticals, biotechnology, and electronics. Two prominent solutions for ACHieving cleanliness are downflow booths and laminar flow booths. While both are designed to minimize contamination, they employ distinct airflow patterns and serve different purposes. Understanding these differences is vital for selecting the appropriate cleanroom equipment for your specific needs.
What is the Difference Between a downflow booth and a laminar flow booth?
Downflow booths and laminar flow booths are both essential for contamination control, but they differ significantly in airflow design and application. downflow booths direct filtered air vertically downward, creating a protective barrier, while laminar flow booths utilize unidirectional airflow that can be either horizontal or vertical to maintain a sterile work environment.
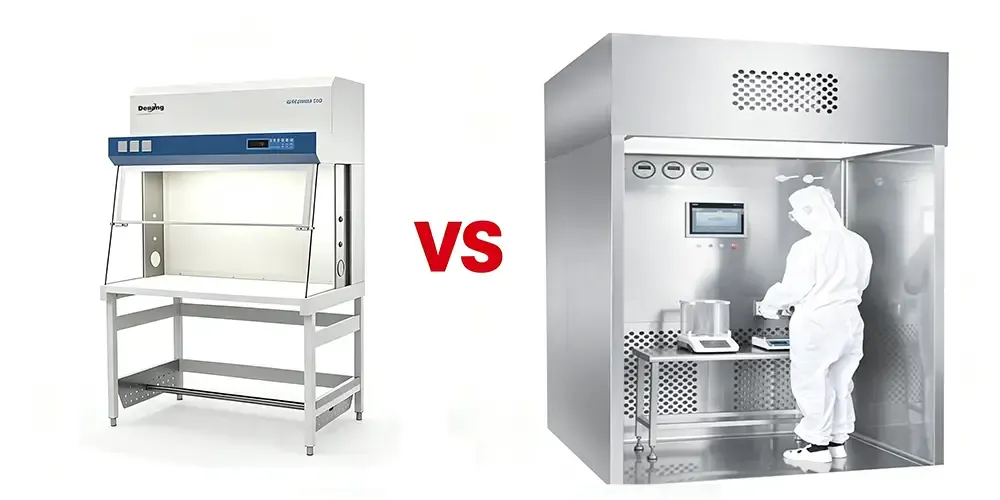
| Feature | Downflow Booth | Laminar Flow Booth |
| Airflow Direction | Vertical downward flow | Unidirectional (horizontal or vertical) |
| Contamination Control | Prevents particles from settling on surfaces | Minimizes turbulence, high cleanliness level |
| Applications | Pharmaceutical compounding, drug formulation | Microbiological work, sterile laboratories |
| Design Features | Can include additional containment features | Varies in size and configuration for different needs |
Airflow Direction
Downflow booths filter air and push it downward, providing a consistent flow that protects the work surface from airborne contaminants. In contrast, laminar flow booths maintain a uniform airflow over the work area, minimizing turbulence and ensuring a consistent clean environment.
Contamination Control
The downflow design is particularly effective at preventing particles from settling on surfaces, making it ideal for sensitive applications like pharmaceutical compounding. Laminar flow booths, while offering high cleanliness levels, require careful design to prevent cross-contamination, especially in laboratory settings.
Applications
Downflow booths are used in environments where direct exposure to contaminants is a concern, such as drug formulation. Laminar flow booths are prevalent in laboratories for microbiological work, where a sterile environment is essential.
Advantages of a Downflow Booth
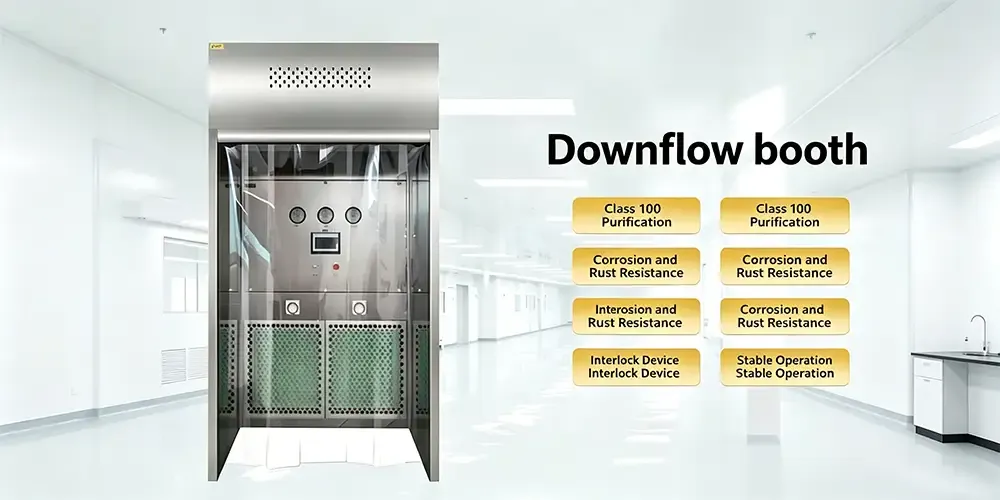
Downflow booths provide numerous advantages in maintaining a contamination-free environment. Their design effectively protects sensitive processes, ensuring high levels of cleanliness. This makes them a preferred choice in various critical applications.
Superior Contamination Control
The vertical airflow in downflow booths creates a protective barrier, significantly reducing the risk of airborne contaminants settling on the work surface. This feature is essential for industries demanding strict cleanliness standards, such as pharmaceuticals and biotechnology.
Versatile Applications
Downflow booths can be tailored for different environments and processes. Whether in drug formulation, electronics assembly, or sterile packaging, these booths deliver effective protection from contaminants. Their design allows for easy integration of additional safety features, such as HEPA filters and UV sterilization, enhancing their functionality and reliability.
How to Control Contamination in a Downflow Booth
Contamination control in a downflow booth involves several key strategies. First, maintaining proper airflow is crucial. This can be achieved through regular monitoring and maintenance of the booth’s filtration system, ensuring that HEPA filters are clean and functioning correctly. Additionally, the use of appropriate personal protective equipment (PPE) is essential for personnel working within the booth to minimize the introduction of contaminants.
Proper cleaning protocols should be implemented, including routine disinfection of surfaces and equipment within the booth. Training staff on best practices for aseptic techniques further reduces contamination risks. Airflow velocity should be regularly assessed to ensure it meets specified standards, typically within the range of 0.45 to 0.60 m/s for effective downflow.
Finally, adhering to relevant domestic and international standards, such as iso 14644 for cleanroom environments and FDA regulations for pharmaceutical manufacturing, ensures that the downflow booth operates within the required cleanliness levels. This comprehensive approach to contamination control helps maintain the integrity of sensitive processes and products.
Functions and Working Principles of a Laminar Flow Booth
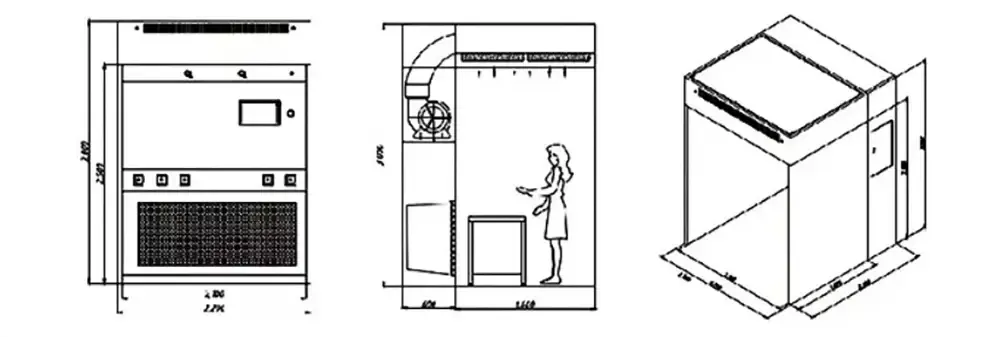
1. Airflow Mechanism
Laminar flow booths utilize a unidirectional airflow system, which moves air in a consistent, parallel stream over the work surface. This design minimizes turbulence and effectively carries away airborne particles, ensuring a clean environment for sensitive work processes.
2. Operational Principles
The operational principle of a laminar flow booth is based on the filtration of air through HEPA or ULPA filters, which trap particles as small as 0.3 microns. The clean air then flows uniformly across the workspace, creating a sterile zone. This design is especially beneficial for tasks like microbiological culture work, where maintaining sterility is critical. Proper airflow management and regular maintenance of filtration systems are essential to ensure optimal functioning and compliance with standards such as ISO 14644 and other relevant guidelines.
Monitoring of a Downflow Booth
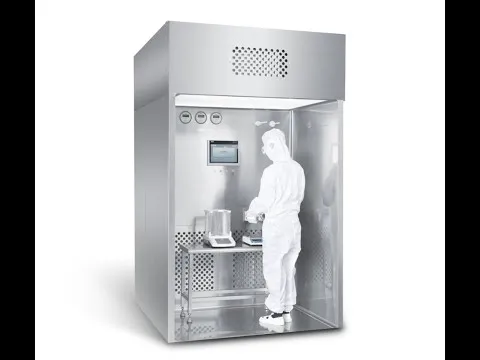
Regular Testing and Validation
Routine testing, including airflow velocity measurements and particle count analysis, should be conducted to verify that the booth operates within specified parameters. This testing should align with guidelines set by relevant standards, such as iso 14644 and FDA regulations. Regular validation processes, including Performance Qualification (PQ) and Installation Qualification (IQ), ensure that the booth consistently meets cleanliness and operational requirements.
Documentation and Record-Keeping
Comprehensive documentation of all monitoring activities is crucial. This includes logs of maintenance, filter changes, and validation tests. Keeping accurate records not only assists in compliance with industry regulations but also provides a historical reference for performance analysis and troubleshooting. By maintaining rigorous monitoring practices, organizations can enhance the reliability of their downflow booths and ensure they meet the stringent demands of cleanroom environments.
Frequently Asked Questions
What distinguishes downflow booths from laminar flow booths?
The distinction lies in their overall purpose rather than just how they create airflows. The purpose of a downflow booth is to use filtered air moving downwards or low-level return or extraction to conserve product from dust contamination during weighing, dispensing, and sampling. A laminar flow booth operates under the principle of directional airflow which can either be horizontal or vertical and helps avoid any airborne contamination, however ensuring that will depend upon the booth's design and functionality.
What are the applications of downflow booths?
Downflow booths can usually be found in such applications as powder weight measurement, raw material sampling, and product dispensing in various pharmaceutical and chemical production stages. In the case of toxic and dangerous powders, one should pay attention to the properties of materials and their safety during operations.
What are the differences between horizontal and vertical laminar airflow?
Horizontal laminar airflow moves through horizontal laminar flow booth from the back of the working area to the front while vertical laminar flows from the filters above down to the working area. Both are meant to protect working stations from anything flying in the air. The choice of the direction depends both on the tasks until the airflow disruption occurs.
Is it possible to use laminar flow booths for all microbiological work?
No. A conventional laminar flow booth is a way to protect the product and does not provide sufficient safety measures and cannot be considered as adequate. When working with agents that cause diseases, possibly contagious agents, or dangerous microorganisms, suitable safety equipment must be chosen according to a biosafety risk analysis.
Are HEPA and ULPA air filters enough to make a work environment completely free of microorganisms?
The answer to the question is no, because HEPA and ULPA filters remove particles that travel through the air; however, filtering alone is not enough to make the environment completely sterile. Other measures must be taken to ensure asepsis along with filtering, including cleaning processes with proven efficiency, operator behaviors, and environment control procedures.
What should be velocity of airflow for downflow booths?
No single airflow velocity complies with all downflow booths. The rate which was provided in the article of 0.45-0.60 m/s should not be viewed as a universal value applied to all situations. Flow of air needs to be established based on various requirements and parameters for given equipment used: nature of powder, conditions of operation, and specific requirements as necessary.
What kinds of monitoring and validation need to be done for downflow booths?
Some common steps in monitoring downflow booths are measuring airflow velocity and volume, conducting airflow visualization, testing filters, controlling pressure differences, and testing alarms. Counting particles can also be required in terms of the specific case; generally, qualification of downflow booths consists of the following.
At what frequency should downflow and laminar air flow booths be checked?
Frequency of maintenance activities must comply with instructions given by the manufacturer and take into account specific features of operation such as the way downflow booth was used, hazards related to substances used in the booth, and the findings from the monitoring conducted.