+86 13638632902
 Jason@cleanroomequips.com


 MENU
Studies show that a facility built around proven key points in cleanroom design delivers 15–20% lower annual operational costs compared to conventional layouts, while maintaining full compliance with global regulatory standards. For engineering and operations teams, balancing strict compliance requirements with long-term cost efficiency is the central challenge of any cleanroom project.
This guide outlines the most important factors in cleanroom design, drawing on decades of Deiiang™ field experience. It serves as a practical cleanroom design checklist that covers everything from initial zoning to long-term maintainability, helping stakeholders make informed decisions during every stage of the cleanroom design process.
Designer's Insight: "The most costly oversight in cleanroom design is ignoring regulatory update headroom — 30% of facilities built before 2020 now require expensive retrofits to meet the latest EU GMP Annex 1 standards." — Jason Peng, Lead Product Designer, Deiiang™ (80+ projects delivered)
Cleanroom Design Process: A Step-by-Step Overview
- Process requirement definition & ISO classification alignment — Match cleanliness class to actual product/process risk.
- Zoning & personnel/material flow path planning — Physically separate flows, establish airlocks and pass-throughs.
- HVAC & filtration system sizing and airflow simulation — Calculate ACH, pressure cascades, and filter coverage.
- Construction material selection and detail design — Specify non-porous, cleanable, chemical-resistant surfaces.
- Commissioning, third-party validation and certification — Verify performance to iso 14644-3 and obtain certification.
8 Key Points: The Expert Checklist
Mastering the essential cleanroom design considerations is critical to delivering a facility that meets performance targets without unnecessary capital or operational spending. These eight cleanroom design best practices represent the core framework used by Deiiang™ engineering teams across pharmaceutical, electronics, and life science projects.
Whether you are evaluating things to consider when designing a cleanroom for a new facility or planning a retrofit, this cleanroom planning checklist will help you align your project with ISO standards, regulatory expectations, and real-world operational needs.
Process-Driven Zoning
Based on extensive Deiiang™ project experience, physical separation of personnel flow and material flow is the foundational logic for preventing cross-contamination. A process-driven zoning strategy maps every step of production, from gowning airlocks to core clean zones, to minimize unnecessary movement and reduce particle generation from human activity.
Personnel routes and material transfer paths are designed to never cross in higher-classification areas, with dedicated pass-through chambers for supplies and separate gowning sequences for staff. This zoning approach is the first item on any rigorous cleanroom design checklist and sets the foundation for all other performance systems.
Inadequate flow separation is a leading cause of FDA GMP observation citations, with shared airlocks increasing cross-contamination risk by up to 40% in ISO 7 zones.
Deiiang Field Data: From 15+ years of on-site engineering experience, shared personnel and material airlocks increase cross-contamination risk by 40% in ISO 7 production zones — a common cost-cutting mistake that leads to validation failure.
Pass-Through
Personnel Only
iso 5 / ISO 7
Separate
HVAC & Energy Efficiency
HVAC systems account for up to 40% of a cleanroom’s total energy consumption, making airflow optimization one of the most impactful cleanroom design tips for long-term cost reduction. Proper air change rates (ACH) and airflow patterns directly impact both cleanliness levels and monthly utility expenses.
- Calculate ACH based on ISO classification: ISO 5 zones typically require 300–500 ACH, while ISO 7 ranges from 60–90 ACH and iso 8 from 20–40 ACH.
- Use low-velocity ceiling diffusers to maintain uniform airflow in critical zones and reduce turbulence that can resuspend particles.
- Implement demand-controlled ventilation to adjust airflow based on real-time particle counts, reducing baseline energy use by up to 18%.
Oversizing AHUs for peak occupancy only creates 25–30% redundant energy consumption during standard operation — a frequent pitfall in retrofit projects.
Pressure Cascade Management
Maintaining a controlled pressure gradient between clean zones is essential for preventing unfiltered air from entering higher-classification areas. This one-way airflow principle is a non-negotiable element of cleanroom design best practices and a core compliance requirement for regulated industries.
Proper pressure cascade design ensures that any air leakage through door gaps or seal imperfections always flows from cleaner to less clean areas, preventing contaminant ingress even during peak personnel traffic.
ISO Classification Alignment
One of the most costly mistakes in the cleanroom design process is over-specifying cleanliness levels. Pursuing ISO 5 for all spaces instead of matching classification to actual process needs can increase capital costs by 35% and inflate long-term energy bills dramatically.
The table below compares relative costs and typical industries across common ISO classifications, based on Deiiang™ project data for 1,000 m² facilities:
| ISO Class | Typical Application | Typical Industries | Relative Capital Cost | Est. Capital Cost per m² | Annual Energy Cost (Baseline = ISO 5) |
|---|---|---|---|---|---|
| ISO 5 | Aseptic filling, wafer fabrication | Pharmaceutical, semiconductor | 100% (baseline) | $4,000 – $6,500 | 100% (baseline) |
| ISO 7 | Compounding, precision assembly | Biotech, medical device, optics | 65% | $2,600 – $4,200 | 55% |
| ISO 8 | Packaging, gowning support | Food, general manufacturing | 40% | $1,600 – $2,600 | 30% |
iso 14644-1 Maximum Allowable Particle Concentrations (particles/m³)
| ISO Class | ≥0.5 μm | ≥5 μm |
|---|---|---|
| ISO 5 | 3,520 | 29 |
| ISO 6 | 35,200 | 293 |
| ISO 7 | 352,000 | 2,930 |
| ISO 8 | 3,520,000 | 29,300 |
≥0.5 μm: 3,520
≥5 μm: 29
≥0.5 μm: 35,200
≥5 μm: 293
≥0.5 μm: 352,000
≥5 μm: 2,930
≥0.5 μm: 3,520,000
≥5 μm: 29,300
cleanroom cost Estimator
Select your parameters to estimate capital cost and annual energy consumption ranges for a new cleanroom.
Estimated Capital Cost:
Estimated Annual Energy Cost:
* Estimates based on Deiiang™ project data for standard cleanroom construction. Actual costs vary with site conditions, utility requirements, and local labor rates. Ranges represent ±25% confidence interval.
Construction Materials
Material selection is one of the essential cleanroom design considerations that directly impacts durability, cleanability, and long-term contamination control. The right materials resist corrosion, minimize outgassing, and withstand repeated disinfection cycles without degradation.
- Wall and ceiling panels: Non-porous, smooth-faced panels with anti-static properties to reduce particle adhesion and support frequent wiping.
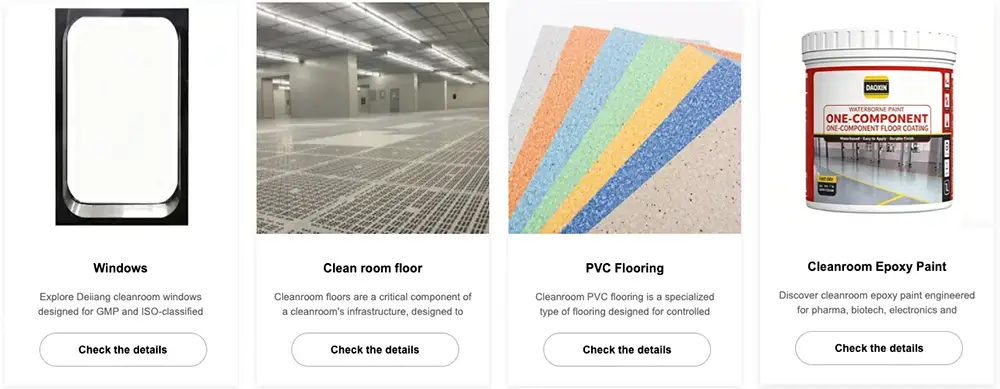
- Flooring: Seamless epoxy or PVC systems with coved corners to eliminate harborage points for microbes and simplify cleaning.
- Fixtures: Stainless steel (SUS 304/316) for work surfaces and pass boxes, resistant to VHP sterilization and chemical cleaners.
Using unsealed gypsum or porous ceiling tiles in clean zones can harbor mold and shed particles, leading to rapid microbial contamination and costly remediation.
HEPA/ULPA Filtration Strategy
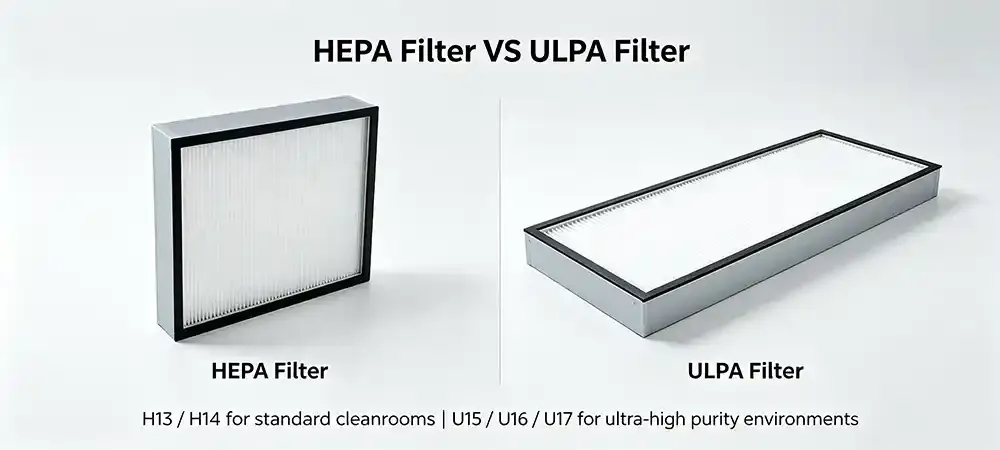
Filter placement and return air design define the effectiveness of your air distribution system, making this one of the most technically important key points in cleanroom design. The layout directly determines particle removal efficiency and airflow uniformity across the workspace.
Top-down supply with side-wall low-level return creates a uniform piston effect that sweeps contaminants downward and out of the clean zone. Filter coverage is calculated using the formula:
Filter Coverage Ratio = (Total Filter Area / Ceiling Area) × 100%
For ISO 5 areas, ceiling coverage of 80–100% with ULPA filters is standard, while ISO 7 zones typically use 25–40% HEPA filter coverage to balance performance and cost.
Refer to IEST-RP-CC034 for HEPA/ULPA filter leak testing and installation requirements.
Smart Monitoring Integration
Real-time environmental monitoring is a core part of the modern cleanroom design process, supporting both audit compliance and proactive maintenance. For FDA- and EMA-regulated facilities, continuous data logging is no longer optional — it is a mandatory compliance requirement.
Integrated particle counters, differential pressure sensors, temperature, and humidity loggers provide continuous data streams that can trigger automated HVAC adjustments and alert staff to deviations before they impact product quality. Deiiang™ designs include centralized monitoring platforms that store records for up to 5 years, simplifying audit workflows and reducing documentation overhead.
Failure to maintain continuous pressure differential data logs is one of the top 10 FDA 483 observation categories for sterile manufacturers.
Maintenance & Expansion
A facility that cannot be serviced or upgraded without full shutdown creates significant long-term operational risk. Modular design with dedicated maintenance access is one of the most underrated cleanroom design best practices, with a major impact on total lifecycle cost.
- Design filter replacement access from the plenum side to avoid disrupting cleanroom operations and requiring re-certification.
- Reserve 10–15% of floor space for future process expansion and utility routing to support capacity growth.
- Use modular wall systems that can be reconfigured without major demolition, reducing renovation time by up to 60%.
Deiiang Field Note: Many contractors quote 3-year HEPA filter service life, but in high-particulate industrial zones with only G4 pre-filtration, actual lifespan drops to 18–24 months. Deiiang designs always include F8 intermediate pre-filters to extend main filter life by 60%.
Compliance Verification & Certification Requirements
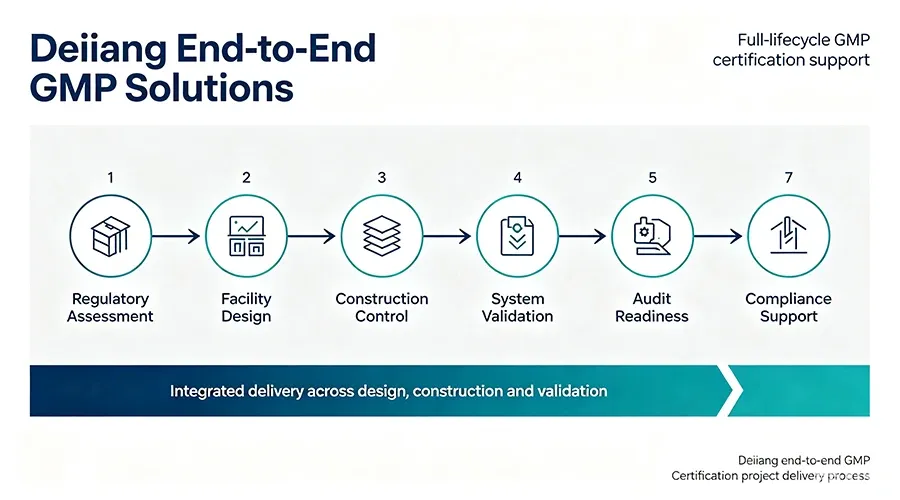
After construction and commissioning, formal validation is required to prove that the cleanroom meets design specifications and regulatory expectations. Third-party certification according to ISO 14644-3 covers tests for airflow velocity, filter integrity, particle count, and pressure differentials. Re-certification is typically required every 6–12 months for GMP facilities, with more frequent monitoring for critical zones.
Ensure all test equipment is calibrated and documentation is traceable. For FDA-regulated spaces, maintain complete validation documentation to support inspections and avoid costly corrective actions.
Deiiang Case Studies
To demonstrate how these cleanroom design tips translate into real-world results, consider the following projects led by Deiiang™ engineering teams.
Biopharmaceutical Cleanroom Retrofit
1,000 m² ISO 7 production zone with ISO 5 aseptic core. BIM prefabrication reduced on-site construction by 30%, and phased installation maintained 75% production capacity. Post-commissioning pressure differentials 12–15 Pa, annual energy 17% below baseline.
Semiconductor Fab Support Cleanroom
800 m² ISO 5 wafer handling area. Integrated AMC filtration and ESD-safe materials. Achieved particle counts 40% below ISO limit. Reduced HVAC energy by 22% through demand-controlled ventilation.
Medical Device Assembly Cleanroom
600 m² iso 7 cleanroom for Class II device assembly. Modular wall system allowed 40% faster reconfiguration for new product line. Passed ISO 14644-3 certification on first attempt.
Common Myths in Cleanroom Design
When reviewing cleanroom planning checklists, many stakeholders fall prey to common misconceptions that drive unnecessary costs and create performance gaps. Below are three pervasive myths and the engineering reality behind each one, based on Deiiang™ field experience across hundreds of projects.
Higher cleanliness ratings are always better.
Over-design is the single largest driver of wasted operational spending. A disciplined cleanroom design process matches classification exactly to process requirements, not to the highest available standard. For non-critical support zones, upgrading from ISO 8 to ISO 7 provides zero measurable quality benefit but increases annual energy costs by approximately 80%.
Over-classifying a facility can inflate capital costs by 35% and lead to unnecessary energy consumption of $50,000+/year for a 1,000 m² facility.Cleanroom construction is a one-time, set-it-and-forget-it investment.
HEPA filters, door gaskets, and sealants all have finite service lives, typically 2–5 years depending on operating conditions. Deiiang™ designs prioritize accessible maintenance paths from the initial planning stage, rather than pursuing maximum airtightness at the expense of serviceability. This reduces filter replacement downtime by up to 50% over the facility lifecycle.
All cleanroom design principles are universally applicable across industries.
Contamination profiles vary drastically by sector. Pharmaceutical cleanrooms focus on microbial control and viable particle monitoring, while electronics facilities prioritize sub-micron particulate control and ESD protection. A design optimized for one industry will rarely perform optimally in another without targeted modifications to address specific contamination risks.
Frequently Asked Questions
For a standard 500–1,000 m² cleanroom, design typically takes 4–8 weeks, construction 8–16 weeks, and commissioning/validation 4–8 weeks. Modular prefabrication can reduce overall schedule by 20–30%. Complex ISO 5 facilities with advanced HVAC may extend to 6–12 months total.
ISO 5 requires 100% ULPA ceiling coverage with laminar airflow (300–500 ACH), while ISO 7 uses 25–40% HEPA coverage and turbulent dilution airflow (60–90 ACH). Capital cost for ISO 5 is roughly 1.5–2.5 times that of ISO 7 per square meter, and energy costs are nearly double.
Top causes include inadequate pressure differentials (below 10 Pa), HEPA filter leaks, insufficient air changes, particle count excursions due to poor airflow patterns, and improper material selection leading to particle shedding. A thorough commissioning plan and pre-testing can prevent most failures.
Yes, many cleanrooms are retrofitted into existing shells. Key considerations include ceiling height for plenum and HVAC, floor flatness, structural load capacity for filters, and utility routing. Modular wall systems and low-profile AHUs make retrofits more feasible, but often cost 15–25% more than new construction per square meter due to constraints.
Micro-Glossary
This quick reference covers key technical terms that appear throughout cleanroom design overview materials and regulatory specifications, helping teams align on terminology during project planning and execution.
- Cleanroom Classification: A grading system defined by ISO 14644 that specifies maximum allowable particle concentrations per cubic meter of air, across defined particle size ranges.
- Laminar Airflow: A uniform, unidirectional airflow state used in the highest classification zones, typically at velocities of 0.3–0.5 m/s to sweep particles away from critical process surfaces.
- Pressure Differential: The static pressure gradient between a cleanroom and adjacent spaces, engineered to prevent contaminant ingress through gaps, doors, and utility penetrations.
- BIM (Building Information Modeling): A digital 3D modeling process that identifies design conflicts before construction begins, reducing on-site rework and improving scheduling accuracy.
Download our full Cleanroom Design Checklist PDF (12-point compliance version) — includes detailed design review forms, ISO classification matrix, and validation test log templates.
Download Free ChecklistReferences
- iso 14644-1:2015 — Cleanrooms and associated controlled environments
- EU GMP Annex 1 — Manufacture of Sterile Medicinal Products
- FDA 21 CFR Part 211 — Current Good Manufacturing Practice
- iso 14644-3:2019 — Test methods